Corrosion-Resistant Stainless Steel Tote Systems for Chemical Manufacturing
Safe, Durable Material Handling Solutions for Corrosive Chemical Processing
Chemical manufacturing presents some of the most demanding material handling challenges in industrial processing. Exposure to aggressive acids, caustic alkalis, solvents, and reactive compounds requires equipment that delivers exceptional corrosion resistance, structural integrity, and operator safety. TOTE® Systems engineers heavy-duty stainless steel tote bins, blenders, discharge stations, and material handling equipment specifically designed to withstand the harsh conditions of chemical production environments.
With over 40 years of experience serving chemical manufacturers, our equipment supports compliance with OSHA Process Safety Management standards, EPA regulations, and industry safety protocols. From bulk chemical storage to precision batching operations, TOTE® Systems delivers the corrosion resistance, containment capability, and reliability chemical processing demands.

Chemical Industry Challenges We Solve
Corrosion from Aggressive Chemicals
Chemical manufacturing facilities handle substances that are highly corrosive to ordinary metals. Acids like sulfuric, hydrochloric, nitric, and phosphoric can rapidly degrade carbon steel and other common materials. Caustic alkalis, oxidizing agents, chlorides, and organic solvents pose additional corrosion challenges. Equipment failure due to corrosion can lead to costly downtime, environmental releases, safety incidents, and contaminated product batches.
TOTE® Solution: Our tote systems are constructed from high-grade 316L stainless steel specifically selected for superior corrosion resistance in chemical processing environments. The addition of molybdenum in 316L provides enhanced resistance to pitting and crevice corrosion, particularly in chloride-containing environments. For extremely aggressive applications, we can engineer systems using upgraded alloys. Electropolished surfaces create a smooth, passive oxide layer that further enhances corrosion resistance and prevents chemical adhesion. All welds are TIG welded to pharmaceutical standards, ensuring no weak points where corrosion can initiate.
Process Safety Management Compliance
OSHA’s Process Safety Management standard requires comprehensive management programs for facilities handling highly hazardous chemicals above threshold quantities. Companies must conduct process hazard analyses, maintain equipment integrity, implement management of change procedures, and document operating procedures. Equipment failures can trigger PSM violations, regulatory citations, and mandatory safety audits.
TOTE® Solution: TOTE® Systems designs equipment that supports PSM compliance requirements. We provide detailed equipment specifications, material certifications, and operating parameters needed for process hazard analysis documentation. Our bins and discharge stations can be configured with safety features including grounding connections for static electricity control, vent connections for pressure relief, containment features to prevent spills and releases, and proper labeling for hazard communication. Equipment is designed for reliable long-term operation, reducing the risk of failures that could compromise process safety.
Hazardous Material Containment and Operator Safety
Many chemical manufacturing processes involve toxic, corrosive, or reactive materials that pose significant health and safety risks to operators. Direct contact with chemicals can cause severe burns, respiratory damage, or systemic toxicity. Even vapor exposure from seemingly minor spills can be dangerous. Traditional open handling methods expose workers to unacceptable risks.
TOTE® Solution: Our material handling systems are engineered with operator safety as a primary design criterion. Sealed discharge valves prevent spillage during material transfer, while integrated dust control systems minimize airborne exposure to powders. Bins can be equipped with vapor-tight covers and gaskets to contain hazardous fumes. Ergonomic design features reduce manual handling requirements, minimizing direct operator contact with materials. Equipment integrates with facility ventilation systems, containment enclosures, and personal protective equipment protocols to create comprehensive safety systems.
Material Compatibility and Product Integrity
Chemical reactions between incompatible materials can cause dangerous incidents including fires, explosions, toxic gas generation, or violent exothermic reactions. Cross-contamination between different chemicals can ruin product batches, requiring costly disposal and facility decontamination. Equipment that has handled one chemical must often be thoroughly cleaned before processing a different material.
TOTE® Solution: Stainless steel’s inert nature provides excellent compatibility with a wide range of chemical substances. Our crevice-free design and electropolished surfaces enable complete cleaning between different product campaigns. Smooth interior surfaces prevent product buildup and facilitate residue removal. Optional color-coding systems, permanent product identification, and dedicated equipment strategies help prevent cross-contamination. We provide detailed cleaning protocols and material compatibility documentation to support your quality and safety programs.
Regulatory Compliance and Documentation
Chemical manufacturers must comply with EPA regulations including RCRA for hazardous waste management, TSCA for chemical substances, and Clean Air Act requirements for emissions. OSHA standards cover worker exposure limits, hazard communication, and personal protective equipment. State and local regulations add additional requirements. Proper documentation is essential for inspections and compliance verification.
TOTE® Solution: TOTE® equipment is designed to support regulatory compliance across multiple standards. We provide material certifications, equipment specifications, and construction documentation needed for facility permits and regulatory filings. Equipment features such as sealed systems, emission controls, and spill containment support environmental compliance. Hazard labeling provisions and safety features align with OSHA requirements. Our documentation packages streamline compliance verification during audits and inspections.
Chemical Industry Applications
Bulk Chemical Storage and Handling
- Raw material receiving and staging
- Intermediate product storage
- Finished product holding and packaging prep
- Specialty chemical handling
- Catalyst and reagent management
- Solvent and carrier liquid storage
Batch Processing and Mixing
- Ingredient weighing and batching
- Multi-component blending operations
- Reaction mixture preparation
- Formulation and compounding
- Product dilution and adjustment
- Specialty blend manufacturing
Powder and Solid Chemical Processing
- Pigment and dye handling
- Catalyst powder management
- Additive and modifier processing
- Precipitated solid collection
- Dried product handling
- Fine chemical processing
Process Chemical Transfer
- Reactor feed systems
- Continuous process material supply
- Batch transfer operations
- Packaging line feeding
- Purification stage transfer
- Waste collection systems
TOTE® Systems Equipment for Food Manufacturing
Heavy-duty 316L stainless steel bins engineered for corrosive chemical handling with capacities from 35 to 110 cubic feet.
Features include:
- 316L stainless steel construction with superior corrosion resistance
- Electropolished finish for chemical compatibility and cleanability
- Sealed butterfly valves prevent spills and emissions
- Grounding connections for static electricity control
- Optional vapor-tight covers with gasket seals
- Fork pockets for facility transport and positioning
- Compatible with containment systems and ventilation

Cost-effective stainless steel bins for less aggressive chemical applications:
Features include:
- Durable 304 stainless steel construction
- Standard discharge valve configurations
- Corrosion-resistant for mild to moderate chemical exposure
- Available in multiple capacities
- Excellent for non-hazardous or packaged chemical handling

Ergonomic access bins that reduce operator exposure during material handling:
Features include:
- Side door access minimizes reaching into bin interiors
- Reduces risk of direct chemical contact
- Gasket-sealed doors prevent chemical vapor escape
- Ideal for sampling and inspection operations
- Facilitates thorough interior cleaning
- Stainless construction throughout

Precision blending equipment for chemical formulation and compounding:
Features include:
- Gentle tumble action prevents material degradation
- Complete discharge minimizes product loss and waste disposal costs
- Sealed construction contains dust and vapors
- Corrosion-resistant materials throughout
- Scalable capacities for various batch sizes
- Easy disassembly for thorough cleaning between campaigns

Controlled chemical transfer systems that enhance safety and efficiency:
Features include:
- Lift and discharge with precise flow control
- Integrated containment catches spills during transfer
- Dust collection connections for powder handling
- Compatibility with receiving vessels and process equipment
- Reduces manual material handling
- Custom configurations for specific applications

Safe elevation and controlled discharge of heavy chemical loads:
Features include:
- Eliminates manual lifting of hazardous materials
- Controlled tilt and discharge rates prevent splashing
- Robust construction handles heavy chemical loads
- Stainless steel for corrosive environment durability
- Integration with downstream process equipment
- Operator controls positioned away from discharge zones

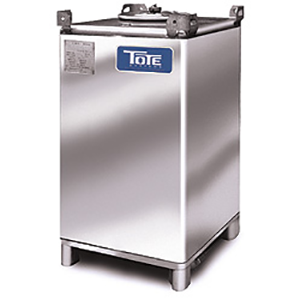
Specialized tanks for liquid chemical storage and transport:
Features include:
- 316L stainless steel construction resists chemical attack
- Available in multiple volume capacities
- Bottom discharge valves for complete emptying
- Forklift compatibility for facility mobility
- Optional heating/cooling jackets for temperature control
- Vapor-tight closures prevent emissions
Dedicated cleaning systems for chemical equipment decontamination:
Features include:
- Complete interior surface cleaning capability
- Efficient rinse and cleaning agent application
- Supports validated cleaning procedures
- Reduces cleaning time between product campaigns
- Captures rinse water for proper disposal
- Chemical-resistant construction throughout

Why Chemical Manufacturers Choose TOTE® Systems
Superior Corrosion Resistance
316L stainless steel with molybdenum provides exceptional resistance to acids, alkalis, chlorides, and oxidizing environments. Electropolished surfaces create a passive oxide layer that further enhances chemical resistance. Our equipment withstands daily exposure to corrosive chemicals that would rapidly destroy ordinary materials.
Process Safety Engineering
Equipment designed with process safety in mind includes features for spill containment, static grounding, vapor control, and emergency venting. Robust construction prevents catastrophic failures. Safety features support OSHA PSM compliance and facility safety programs.
Durable Construction for Harsh Environments
Chemical plants are demanding environments with frequent washdowns, temperature variations, and exposure to cleaning agents. TOTE® bins are built to last through decades of service in these conditions. Heavy-gauge stainless steel construction, reinforced frames, and industrial-grade components ensure long equipment life.
Customization for Specific Chemicals
Every chemical has unique handling requirements. We customize bin internals, discharge configurations, surface treatments, sealing systems, and materials of construction to match your specific chemical compatibility needs. Whether handling concentrated acids, caustic solutions, or aggressive solvents, we engineer appropriate solutions.
Comprehensive Safety Documentation
We provide material safety data, chemical compatibility information, equipment specifications, operating guidelines, and cleaning procedures to support your safety and training programs. Documentation packages assist with PSM compliance, hazard communication requirements, and facility safety protocols.
Reduced Total Cost of Ownership
Stainless steel equipment represents a higher initial investment compared to carbon steel or coated alternatives, but delivers significantly lower lifetime costs. Superior corrosion resistance eliminates premature failures and replacement costs. Minimal maintenance requirements reduce downtime. Long service life means decades of reliable operation from a single equipment investment.
Chemical Processing Standards and Features
Material Selection for Chemical Resistance
- 316L stainless steel with 2-3% molybdenum for enhanced corrosion resistance
- Electropolished surfaces provide smooth, passive oxide layer
- TIG welded construction eliminates corrosion initiation points
- Optional upgraded alloys (904L, Alloy 20, duplex stainless) for extreme applications
- Documented material certifications traceable to mill test reports
Safety and Containment Features
- Grounding lugs and connections prevent static electricity buildup
- Vapor-tight covers with chemical-resistant gaskets
- Secondary containment provisions for spill control
- Vent connections for pressure relief and emission control
- Hazard labeling provisions for chemical identification
- Safety interlocks available for automated systems
Chemical Compatibility Design
- Smooth, non-porous surfaces prevent chemical absorption
- Crevice-free construction eliminates entrapment areas
- Complete drainability prevents residue accumulation
- Compatible gaskets and seals for specific chemicals
- Easy disassembly for inspection and maintenance
Process Integration Capabilities
- Standard and custom discharge configurations
- Compatible with reactors, mixers, and process vessels
- Integration with facility ventilation systems
- Automation-ready with sensor mounting provisions
- Scalable from pilot plant to full production volumes
Chemical Industry Segments We Serve
TOTE® Systems provides material handling solutions across the chemical manufacturing spectrum:
- Commodity Chemicals: Sulfuric acid, caustic soda, ammonia, chlorine compounds
- Specialty Chemicals: Catalysts, surfactants, polymer additives, performance chemicals
- Agricultural Chemicals: Pesticides, herbicides, fertilizers, soil amendments
- Industrial Chemicals: Solvents, cleaning agents, processing aids, intermediates
- Coating and Adhesive Chemicals: Resins, hardeners, pigments, additives
- Water Treatment Chemicals: Coagulants, flocculants, disinfectants, pH adjusters
- Petrochemicals: Refining catalysts, process chemicals, additives
- Fine Chemicals: High-purity compounds, pharmaceutical intermediates, research chemicals
Safety and Regulatory Support
OSHA Compliance
Equipment designed to support compliance with:
- Process Safety Management (29 CFR 1910.119)
- Hazard Communication Standard (29 CFR 1910.1200)
- Personal Protective Equipment requirements
- Lockout/Tagout procedures
- Confined space entry protocols
EPA Compliance
Features supporting environmental regulations:
- Spill containment and secondary containment
- Emission control provisions
- Waste minimization through complete discharge
- Material compatibility for hazardous waste handling
Industry Standards
Design and construction aligned with:
- ASME codes for pressure vessels where applicable
- NFPA standards for fire prevention
- API recommendations for chemical storage
- Industry best practices for safe chemical handling
Get Started with Chemical-Grade Tote Systems
Whether you’re processing commodity chemicals in high volumes or manufacturing specialty compounds with stringent purity requirements, TOTE® Systems delivers material handling equipment engineered for the demanding conditions of chemical manufacturing.
Contact TOTE® Systems today:
- Phone: 1-888-838-4178
- Request a Quote: Custom chemical handling solutions
- Discuss Your Project: Application-specific design consultation
From raw material receiving through finished product packaging, TOTE® Systems keeps your chemical manufacturing operation safe, efficient, and compliant.
People Also Ask
316L stainless steel provides excellent resistance to many acids including sulfuric acid (moderate concentrations), phosphoric acid, acetic acid, and citric acid. For highly concentrated acids or elevated temperatures, we can specify upgraded alloys like 904L or Alloy 20. We recommend providing specific details about your chemical, concentration, and temperature for proper material selection.
Our electropolished stainless steel surfaces facilitate cleaning with appropriate solvents, detergents, or cleaning agents. The specific cleaning method depends on the chemical residue being removed. We can recommend cleaning protocols based on your application and provide validation support if needed.
While PSM compliance is facility-specific and depends on your complete process, our equipment is designed with PSM principles in mind. We provide detailed specifications, material documentation, operating parameters, and safety feature descriptions needed for PSM documentation, process hazard analysis, and equipment integrity programs.
Absolutely. Our tote systems integrate with automated material handling, weighing systems, batch controls, and process automation. We can configure equipment with load cells, level sensors, automated valves, and control interfaces to match your automation requirements.